Blog : A new approach to tirage bin loading
Hill-Smith Family Estates
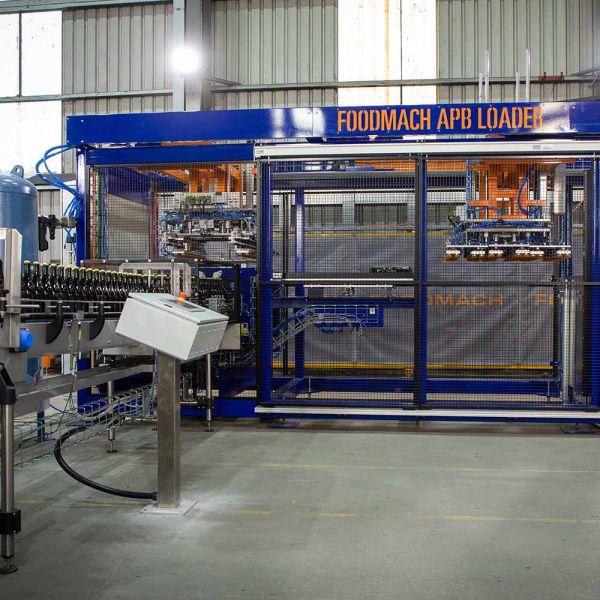
Foodmach developed a purpose-built loading system for Hill-Smith Family Estates, tailored to its bottle-handling process and the space available within its existing tirage line.
Background
Hill-Smith Family Estates (HSFE) called Foodmach in to assess a bottle-handling challenge in its traditional-method sparkling wine production.
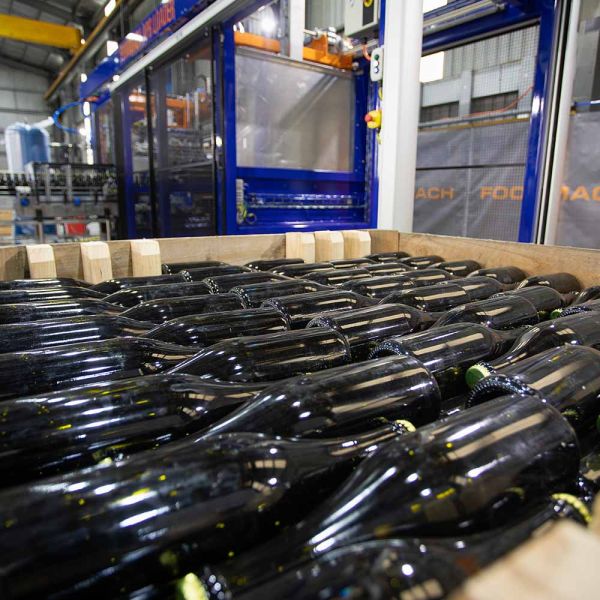
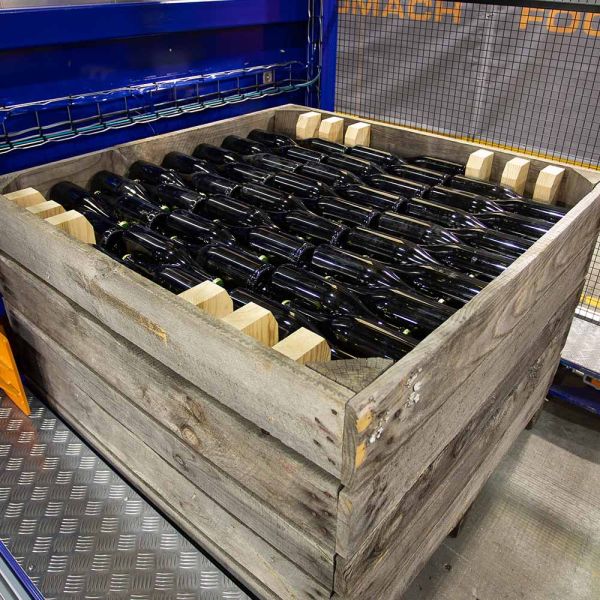
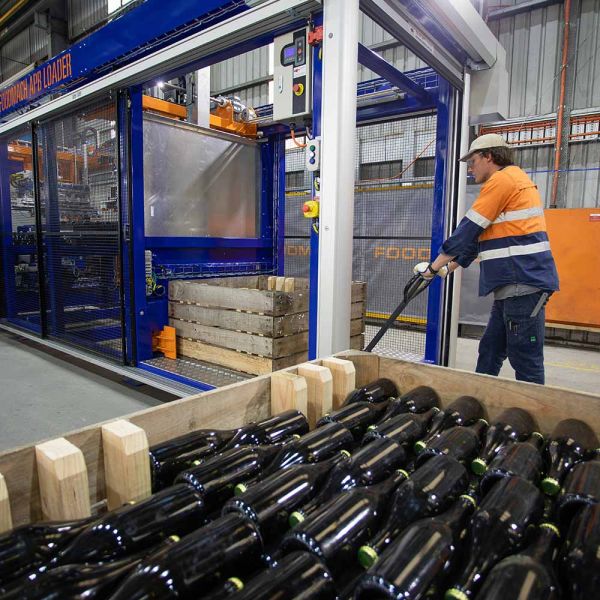
Loading bottles into timber tirage bins was a manual process with precise requirements. Bottles needed to move from upright to horizontal, form an interlocking pattern and be placed in complete layers for secondary fermentation and storage.
Foodmach worked with HSFE to develop a bespoke approach. The teams agreed on a fixed price for the defined scope, giving HSFE cost certainty for the development.
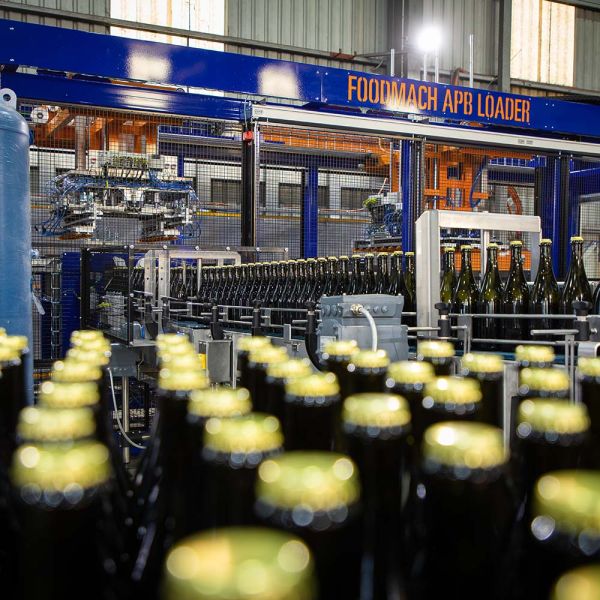
The resulting Automatic Pallet Bin (APB) Loader was designed and manufactured at Foodmach’s Echuca facility, with a design capacity of up to 5,500 bottles per hour.
It has successfully completed Factory Acceptance Testing (FAT), with site installation and commissioning to follow.
A precise bottle-handling sequence
Automating the process meant controlling every bottle through a sequence of movements while maintaining the required packing pattern.
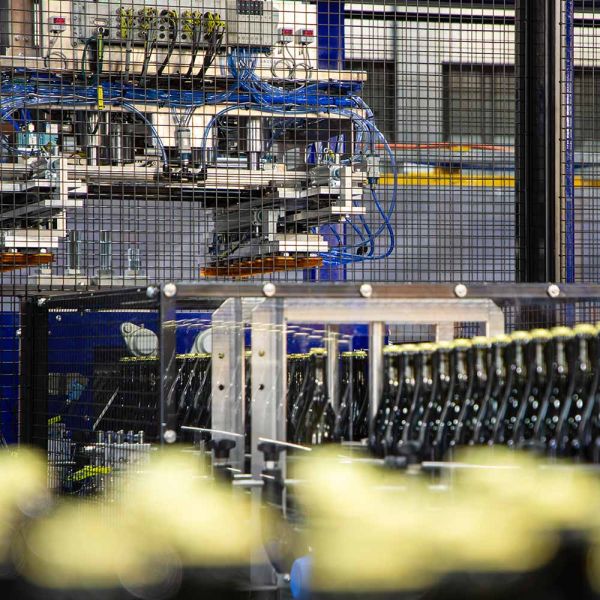
The system needed to count and group incoming bottles, turn them horizontally and nest them into stable rows. It then had to place each complete layer inside a timber bin at the correct height, repeating the sequence until the bin was full.
Protecting bottle integrity throughout the process was essential. The loader also needed to accommodate both bottle types and provide controlled access for operation and maintenance.
Key objectives for the project were:
- Improved ergonomics: reducing the physical demands of repetitive bottle handling.
- Reduced manual-handling risk: automating the loading of bottles into timber tirage bins.
- Higher throughput: developing a system designed to handle up to 5,500 bottles per hour.
From production requirements to a purpose-built machine
Foodmach brought its mechanical engineering, manufacturing and controls teams together to develop a coordinated loading system around HSFE’s requirements.
Forming the bottle layers
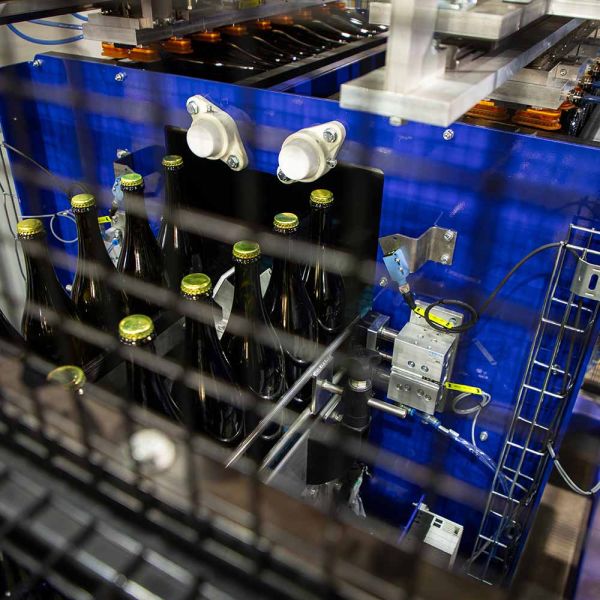
Bottles arrive upright from the production line, divide into two lanes and accumulate into programmed groups.
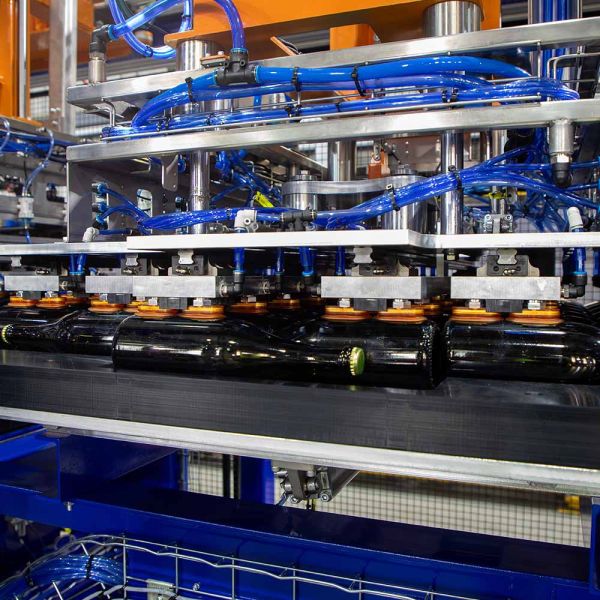
A controlled orientation mechanism turns them horizontally before the staging system positions and nests them into interlocking rows.
Three rows combine to form each complete layer.
Loading the timber bins
A transfer mechanism places the completed layer into the bin at the required height and position.
Loading continues automatically until the programmed layer count is reached, then the system signals for a bin change.
Managing the sequence
Foodmach developed the electrical and software package alongside the mechanical system.
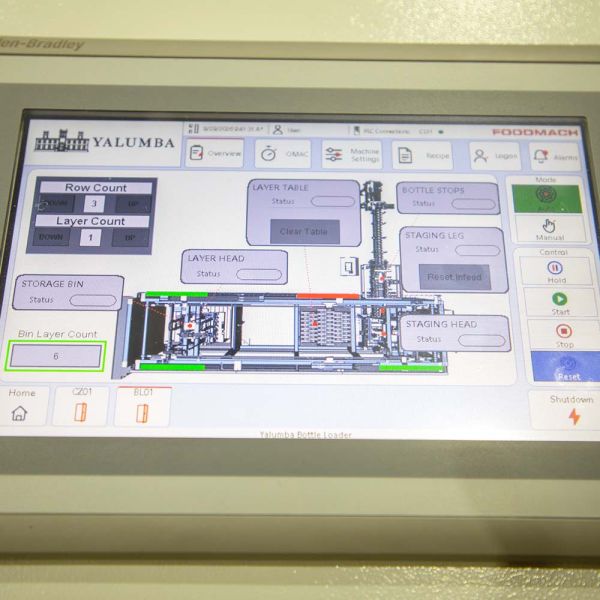
Operators use a central HMI for recipe selection and machine operation, with diagnostics and alarms to support fault finding.
Perimeter guarding and monitored access points are integrated with the machine’s safety controls.
Factory-tested before installation
The complete system was assembled and factory-tested at Echuca, bringing the bottle-handling mechanisms and control sequence together before site installation.
This is a critical step in Foodmach’s Vertical Startup System towards production readiness.
It provides an opportunity to assess the integrated system before it reaches the customer’s line and supports a more controlled installation and commissioning process.
The loader has successfully completed FAT. Sustained production performance will be confirmed following commissioning at HSFE.
One engineering partner responsible for delivery
HSFE needed equipment tailored to its process and factory layout. Foodmach took responsibility for developing that solution within an agreed scope and fixed price.
With design, manufacturing and controls delivered in-house, Foodmach carries responsibility for the complete system through to installation and commissioning.
HSFE has one engineering partner accountable for turning the production requirement into working equipment and integrating the loader into its existing tirage line.
Customer: Hill-Smith Family Estates (HSFE)
Application: Tirage bottle handling and timber-bin loading
Bottle types: Heavy wine and sparkling bottles
Solution: Foodmach Automatic Pallet Bin Loader
Commercial approach: Bespoke development for an agreed fixed price
Design capacity: Up to 5,500 bottles per hour
Scope: Design, manufacture, electrical and software, FAT, installation and commissioning
Project status: FAT completed; site installation and commissioning to follow
Have a production challenge that needs a tailored solution?
Talk to Foodmach about what you need to achieve.